
Use Progressive Die Stamping when a repeat part can move through a defined carrier-strip sequence. The specialist page covers station logic and repeat production decisions.
Learn More 


Send the current drawing and CAD where available. State material grade, thickness or strip condition, formed views, critical dimensions and datums, finish, mating parts, expected demand, revision status, inspection requirements and packing condition. A sample helps when it explains function or receiving condition better than a drawing.
| RFQ input | What to provide | Decision it supports |
| Drawn geometry | Installed orientation, load or contact function, mating part and protected surfaces. | Which formed features are functional and how they should be accepted. |
| Material and form | Grade, thickness, temper, coil/sheet condition and finish requirement. | Formability, springback, edge condition and surface protection. |
| Geometry and process | Flat and formed views, holes, bends, draw depth, tabs, threads and secondary work. | Whether the part fits progressive, transfer, fine blanking, four slide or deep drawing. |
| Program context | Demand, prototype stage, drawing revision and repeat-supply expectation. | Tooling route, validation plan and commercial comparison. |


These are drawing-review checkpoints, not general capability claims. The selected process and final result must be confirmed from actual geometry, material and production requirements.
| Characteristic | Project reference | Confirmation needed |
| Input form | The part may begin as coil, strip, sheet blank or a transferred workpiece. | Material condition, feed logic, grain direction and supplied surface. |
| Forming route | The part may be cut, pierced, bent, formed, drawn or finished across one or more stages. | Feature order, access, springback, draw severity and secondary work. |
| Functional features | A stamped part may locate, retain, protect, connect, contact or support another component. | Mating geometry, load/contact condition and inspection datum. |
| Program release | A production route must account for tooling, revisions and the required delivered condition. | Sample evidence, revision approval, packing and repeat-order controls. |


Stainless steel, carbon steel, aluminum, brass, copper alloys and another drawing-specified material behave differently in cutting, bending, forming, drawing and finishing. State the function first: corrosion resistance, conductivity, spring action, wear, visible surface, sealing or structural support. Then define the secondary work needed to deliver that condition.
Identify burr-sensitive edges, critical bends, contact surfaces and areas needing coating, plating, deburring, joining or protected packing. This keeps the quotation aligned with the assembly rather than a generic stamped shape.
Related manufacturing routes
Where a project combines stamped parts with machined interfaces, CNC Machining Service can support the related solid-stock requirement. Define which datum and condition transfer between processes.


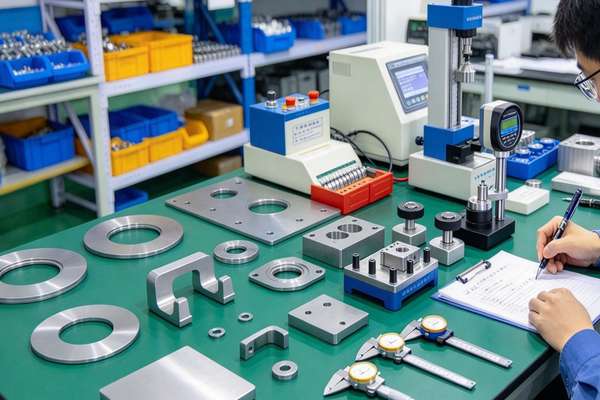
An effective plan identifies the edge, hole, bend, formed feature, surface or datum that governs assembly performance. Provide the approved drawing revision, material and finish requirement, acceptance evidence and packing condition needed by receiving.
The suitable process depends on the material input, geometry, forming directions, functional edges, hollow features and expected program. Hardware SP can review a drawing to compare progressive, transfer, fine blanking, four slide, deep drawing or another route before tooling is selected.
Provide a drawing or CAD file, material and thickness, formed views, critical dimensions and datums, finish, mating condition, expected demand, revision status, inspection needs and packing requirement. A sample helps where it shows function or receiving condition more clearly.
Progressive stamping may fit when the part can remain carrier-supported through a repeat sequence and the program supports dedicated tooling. The decision depends on actual geometry, material and demand. Review the drawing before assuming a process from volume alone.
Yes. Piercing, trimming, deburring, joining, threading, machining, coating, plating and packing may be needed for an assembly-ready component. Define the final condition and protected interfaces so those operations are included in the process review rather than treated as an undefined handover.
It depends on the part, its stage and whether production tooling will support repeat demand. For an early or lower-volume project, the review should compare tooling exposure with alternate routes and clarify what evidence is needed before a production tool is released.