Use Progressive Die Stamping when a stable carrier strip and repeat station sequence suit the finished part. Four slide becomes relevant when the forming directions and compact geometry make a multi-slide approach worth reviewing.

English 


Send the current drawing, CAD where available, and a sample when it explains function. Define material and strip/wire condition, thickness or diameter, bend directions, critical gaps, contact or retention function, finish, assembly relationship, demand and revision status. These inputs show whether multi-directional forming is genuinely useful.
| RFQ input | What to provide | Decision it supports |
| Form geometry | Bend views, wrapped features, cutoffs, tabs, holes and the installed orientation. | Whether multiple slides create a useful forming route. |
| Material condition | Strip or wire form, grade, thickness or diameter, temper, coating and spring requirement. | Formability, springback discussion and later finish planning. |
| Functional use | Retention load, contact point, routing path, mating part and allowable movement. | Which features are functional and which dimensions need controlled acceptance. |
| Program context | Demand, sample stage, revision risk and repeat supply expectation. | Tooling comparison, validation plan and total-program decision. |
| Secondary work | Plating, heat treatment, joining, insertion, marking or packaging needs. | A defined handover condition and fewer supplier-to-supplier assumptions. |


These are drawing-review checkpoints, not general capability claims. Final process fit, achievable result and tooling route must be confirmed from the part geometry, material and program requirements.
| Characteristic | Project reference | Confirmation needed |
| Part starting form | The part may start from strip or wire before forming and cutoff. | Material form, feed direction, supplied condition and allowable marking. |
| Formed features | Bends, wraps, tabs and contact arms may be formed from multiple directions. | Sequence, inside condition, springback, access and mating geometry. |
| Functional movement | A formed feature can retain, route, contact, flex or locate another component. | Installed position, deflection, load path and acceptance criterion. |
| Secondary condition | Finish or joining can alter the condition delivered to assembly. | Plating, heat treatment, joining, deburring and packing orientation. |
| Tooling decision | A dedicated route should be assessed against total program needs. | Demand, revision risk, prototype evidence and alternative process comparison. |

Use Progressive Die Stamping when a stable carrier strip and repeat station sequence suit the finished part. Four slide becomes relevant when the forming directions and compact geometry make a multi-slide approach worth reviewing.

A multi-slide route may deserve separate evaluation when the drawing needs more forming directions, restricted feature access or additional operations beyond a basic four-slide sequence. Do not select by the process label alone. Compare the actual feature order, input form, material response, secondary work and revision exposure before a tooling route is chosen.

Link to Metal Stamping for the broader sourcing context. The link should help a buyer compare manufacturing routes, not add every stamping keyword to one page.

If the component needs a later precision interface, fixture feature or related solid-stock part, CNC Machining Service can support a combined sourcing discussion. Define the datum passed from the formed part to the next process.
Choose material by installed function. Stainless, carbon or spring steel, brass, copper alloys and drawing-specified alternatives behave differently in bending, contact, resilience and finishing. State material form, temper, coating and the functional surface so the review covers the delivered component—not only the raw material name.
State where electrical contact occurs, whether plating is specified and what must remain protected through handling and assembly.
Describe the installed position, required movement and mating part rather than relying on an unsupported generic spring claim.


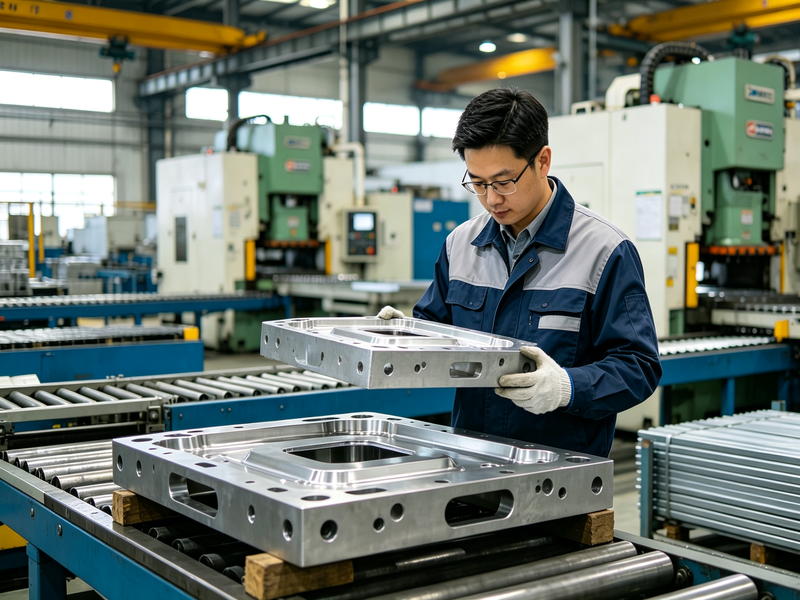
A useful inspection plan identifies the formed angle, contact or retention region, critical gap, hole or cutoff, and the datum used to judge installed position. Include first-sample evidence, material information, finish requirement and packing orientation where they affect receiving.
Ask when a compact strip- or wire-based component needs features formed from more than one direction. Hardware SP reviews the drawing, material condition, installed function, demand and secondary work before comparing four slide with progressive or another route. Make that decision before fixing a tool concept.
Provide drawing or CAD, material form and specification, thickness or wire diameter, formed views, critical gaps, functional contact or retention details, finish, assembly context, demand and revision status. Include a sample if it explains the installed action better than the drawing.
Four-slide tooling approaches compact features from multiple directions. Progressive stamping usually advances a carrier-supported strip through stations. Either can fit; select from geometry, material, forming access and program needs—not from the process name in an RFQ.
It can be reviewed for clips, contacts, terminals, flat springs and related parts when material behavior, contact or retention function, and bend sequence fit the route. Provide mating context, material, finish and installed orientation so the whole interface can be assessed.
Issue a clearly identified revised drawing and state which formed feature changed. Material, bend direction, gap, contact location, finish or orientation can affect tooling, inspection and packing. Hardware SP should review the effect before tool release or alteration, then align sample evidence to the approved revision.