A custom aluminum extrusion is selected when the same cross-section must carry a functional channel, enclosure wall, heat path, mounting face or structural relationship along its length. The procurement risk is often created after the profile is chosen: an undefined cut length, weak machining datum, missed finish boundary or unsuitable packout. This page keeps those decisions together.
Send the profile cross-section, finished-part drawing, CAD, alloy/temper requirement if specified, finished length, quantity, surface requirement, machining/fabrication detail, revision and packing requirement. If you have only a concept, identify the functional faces, channels, assembly connection and target receiving condition for a feasibility review.
| RFQ input | What to provide | Decision it supports |
| Profile definition | Cross-section drawing, wall/channel features and functional faces. | Profile feasibility and tooling discussion. |
| Finished part | Cut length, end condition, holes, slots, tapping, milling or assembly features. | Post-extrusion manufacturing scope. |
| Material and finish | Specified alloy/temper, visible surface and coating/anodizing requirement if applicable. | Finished-condition and protection review. |
| Programme context | Sample/production need, quantity, revision and packing requirement. | Tooling, quote and repeat-supply reference. |


These are drawing-review checkpoints, not generic capability claims. Final alloy, temper, profile feasibility, tooling, tolerances, finishing and delivery condition require confirmation from the actual project.
| Characteristic | Project reference | Confirmation needed |
| Profile cross-section | A profile may contain channels, cavities, wall transitions or mounting features. | Functional section, drawing revision and tooling scope. |
| Length and end condition | The part may require a defined cut length, end preparation or protected finish. | Finished length, datum and receiving condition. |
| Post-extrusion features | A profile can need holes, slots, threads or machined interfaces. | Feature drawing, datum relationship and final assembly function. |
| Component set | Profiles may ship with fasteners, inserts, brackets or protective accessories. | Set contents, count, hardware condition and packing. |
For local drilled, tapped or milled interfaces, see CNC Machining Service. For sheet-metal brackets or covers that join the profile assembly, see Sheet Metal Assembly. For connecting hardware, see Custom Fasteners. Add live links after destination URLs are verified.
Define what the section must do across its full length: guide, enclose, mount, dissipate, support or connect.
Use the controlled cross-section, expected programme and project requirements to determine the tooling discussion before production release.
Specify cut length, required follow-on work, finish protection, included hardware and packing for your receiving process.
The profile drawing should identify the project-specified alloy and temper, together with visible surfaces, contact points, environmental exposure and any required surface finish. If anodizing, powder coating, machining exposure or cosmetic consistency matters, state the governed requirement and which faces it applies to. “Aluminum” alone does not release a finished extrusion component.
Longer profile components can be damaged at ends, visible faces or machined features during handling. Define separation, orientation, labels, end protection and kit contents around how the parts are received and assembled. This makes packing part of the technical scope rather than an afterthought.


Build this cluster with Stainless Steel Fastener Material Guide, Stainless Steel Fasteners and Galling Guide and an approved Stainless Steel Fastener Case Study after those pages are published and URLs verified.
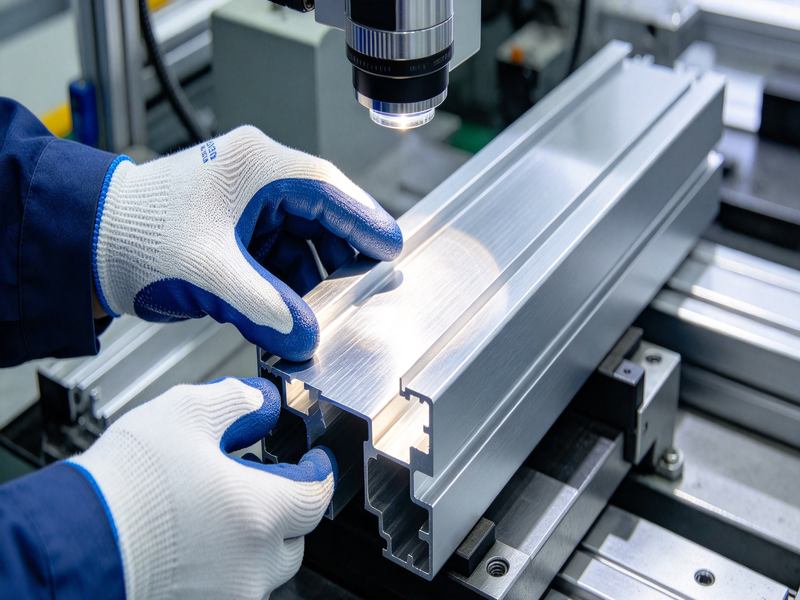
Release should focus on the controlled section, finished length, functional faces, specified local features, alloy/temper requirement, surface condition, included components and protected packing. Provide the approved revision and receiving evidence.
Provide the cross-section drawing, finished-part drawing or CAD, material requirement, target length, post-extrusion features, finish, quantity, revision and packing requirement. The cross-section and the final part should both be visible, because continuous profile geometry and local fabrication features are different decisions.
A new cross-section normally needs a profile-tooling discussion. The final decision depends on the approved section, functional geometry, programme context and supplier review. Send the cross-section, expected quantity and finished-part requirement so tooling can be assessed as a project decision rather than assumed from an image.
Show every local hole, slot, tapped feature, end detail and its datum relationship to the profile. The extrusion drawing establishes continuous geometry; the finished-part drawing defines downstream work. This separation makes quotation and quality release more reliable.
Use the alloy/temper called out by the drawing or project specification. Also state the intended environment, visible-surface requirement, connected materials and any finishing requirement. If the selection is not final, send the operating need and flag the material decision for review.
Specify part length, visible and machined surfaces, end protection, separation, bundle or kit count, labels and receiving method. Long profiles can be affected by handling, so packing should be part of the quote scope when surface condition or downstream assembly matters.
Hardware-SP can assess B2B drawing-led projects where the profile, finished-part requirement and receiving condition are defined by drawings, samples or technical requirements. We review feasibility, quote, manufacture, control quality and ship against the confirmed requirement. Final route and acceptance details depend on the actual project information.